
BGA soldering yield under 80% – what are the solutions?
2026-08-18
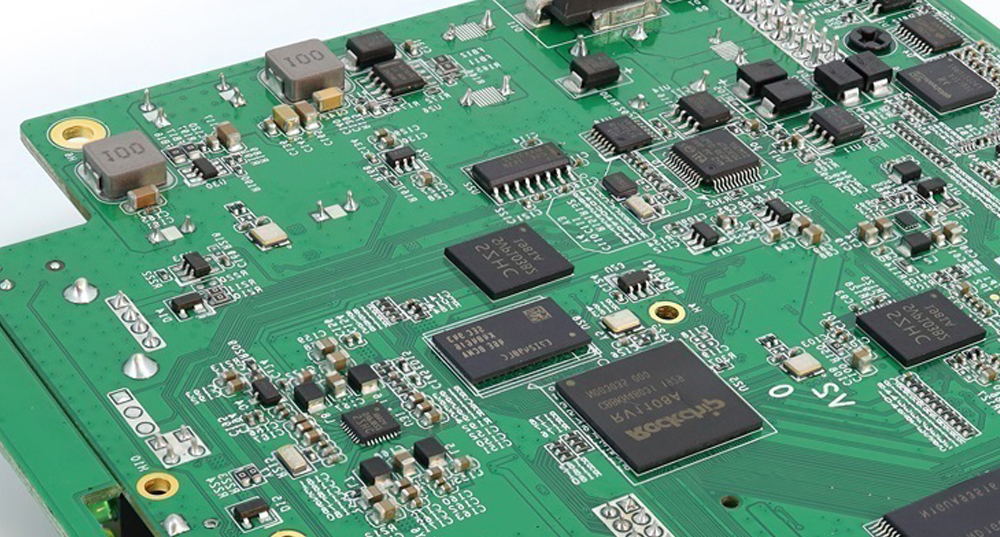
If you've worked with BGA boards, you've probably been there: the boards come off the line, and you run functional test — 20% of them fail. Open joints. Shorts. Intermittent signals.
You've already spent good money on design and components. Now a fifth of your boards are scrap. And the thing is, this isn't rare. Many factories simply can't get BGA yield above 80%.
A yield below 80% means one in five boards needs rework. And reworking a BGA board isn't just "re-solder it and done." You have to remove the chip, clean the pads, re-ball, re-place, and reflow again. That's a lot of labor and time — more than soldering a new board. Worse, the reliability of a reworked BGA is never the same. The solder joints have already been through one thermal cycle. The pads may have been damaged during removal. Some boards work right after rework but fail weeks later in the field — those intermittent failures are the hardest to track down.
So BGA assembly isn't just "put it on and hope for the best." It has its own rules.
Why Is BGA Yield So Hard to Get Right?
1. Solder Paste Printing
Solder paste thickness, shape, and position — if any of these are slightly off, the BGA balls won't align with the pads. BGAs have many pins in a tight pitch. If the stencil aperture isn't designed right, paste viscosity is off, or printing pressure fluctuates, the paste volume becomes inconsistent. Too much paste causes bridging; too little causes open joints.
Solder paste thickness, shape, and position — if any of these are slightly off, the BGA balls won't align with the pads. BGAs have many pins in a tight pitch. If the stencil aperture isn't designed right, paste viscosity is off, or printing pressure fluctuates, the paste volume becomes inconsistent. Too much paste causes bridging; too little causes open joints.
2. Reflow Profile
BGAs are sensitive to temperature. Heat up too fast, flux doesn't activate properly and voids don't escape. Cool down too fast, the solder joints develop internal stress. Every BGA has its own recommended reflow profile. One profile does not fit all.
BGAs are sensitive to temperature. Heat up too fast, flux doesn't activate properly and voids don't escape. Cool down too fast, the solder joints develop internal stress. Every BGA has its own recommended reflow profile. One profile does not fit all.
3. Placement Accuracy
If the mounter is misaligned or the placement pressure is wrong, the BGA balls won't sit properly on the pads. Reflow will shift or bridge them.
If the mounter is misaligned or the placement pressure is wrong, the BGA balls won't sit properly on the pads. Reflow will shift or bridge them.
4. Moisture Control
BGAs are moisture-sensitive. Left exposed, they absorb moisture from the air. If you don't bake them before reflow, the moisture expands under heat and creates voids inside the balls — visible as dark spots on X-ray. Voiding above 25% is
BGAs are moisture-sensitive. Left exposed, they absorb moisture from the air. If you don't bake them before reflow, the moisture expands under heat and creates voids inside the balls — visible as dark spots on X-ray. Voiding above 25% is
unacceptable.
How to Improve BGA Yield
1. Use X-Ray for Process Monitoring
Don't wait until the whole batch is done to discover defects. Best practice: inspect the first board off the line with X-ray — check ball shape, voiding, bridging. Once the process is stable, run the batch and spot-check every 2 hours. This catches drift early, so you can intervene before it becomes a field failure.
Don't wait until the whole batch is done to discover defects. Best practice: inspect the first board off the line with X-ray — check ball shape, voiding, bridging. Once the process is stable, run the batch and spot-check every 2 hours. This catches drift early, so you can intervene before it becomes a field failure.
2. Fine-Tune Your Reflow Profile
Use a thermal profiler to measure actual board temperature. The BGA solder joint needs to reach its melting point for long enough — but not too long. Solder paste suppliers provide baseline profiles; you need to adjust based on your board's thermal mass. Boards often have different thermal profiles at different locations — edge vs center — so you need to place thermocouples in multiple positions and verify they all stay within the process window. This step is often overlooked but critical.
Use a thermal profiler to measure actual board temperature. The BGA solder joint needs to reach its melting point for long enough — but not too long. Solder paste suppliers provide baseline profiles; you need to adjust based on your board's thermal mass. Boards often have different thermal profiles at different locations — edge vs center — so you need to place thermocouples in multiple positions and verify they all stay within the process window. This step is often overlooked but critical.
3. Strict Moisture Control
After opening, BGAs must be used within floor life (usually 48 hours) or baked before assembly — 125°C for 8–12 hours. Keep workshop humidity at 30–60% RH. It's a hassle, but skipping this step means voiding, and X-ray will catch every single one.
After opening, BGAs must be used within floor life (usually 48 hours) or baked before assembly — 125°C for 8–12 hours. Keep workshop humidity at 30–60% RH. It's a hassle, but skipping this step means voiding, and X-ray will catch every single one.
If you're looking for a BGA-capable PCBA partner, or if your current factory can't get the yield right, send us a photo of your board and the BGA part number. We can tell you — what to watch out for on your specific board, and what yield you should expect.
Why Choose Nano Coating for PCBA Waterproofing?
Why Does PCBA Cost So Much?


SEND MESSAGE